What you’ll learn in this article:
- How processing efficiency directly determines how much you’re paying per tonne, and what to optimise first
- Why material resale value is a recoverable revenue stream
- How equipment uptime is the hidden lever behind both cost control and throughput performance
When waste management operators look to cut costs, the instinct is often to renegotiate collection contracts or reduce frequency. But the most effective cost reductions rarely happen on the road, they happen on-site, in the way material is processed, sorted, and recovered before it ever leaves the facility.
The operators consistently achieving lower cost-per-tonne figures are focused on three areas: how efficiently material moves through their facility, how much they recover from resale, and how reliably their equipment performs.
Get those three right, and you reduce costs without touching your collection schedule at all.
Processing Efficiency: Where Cost Leaks Are Hiding
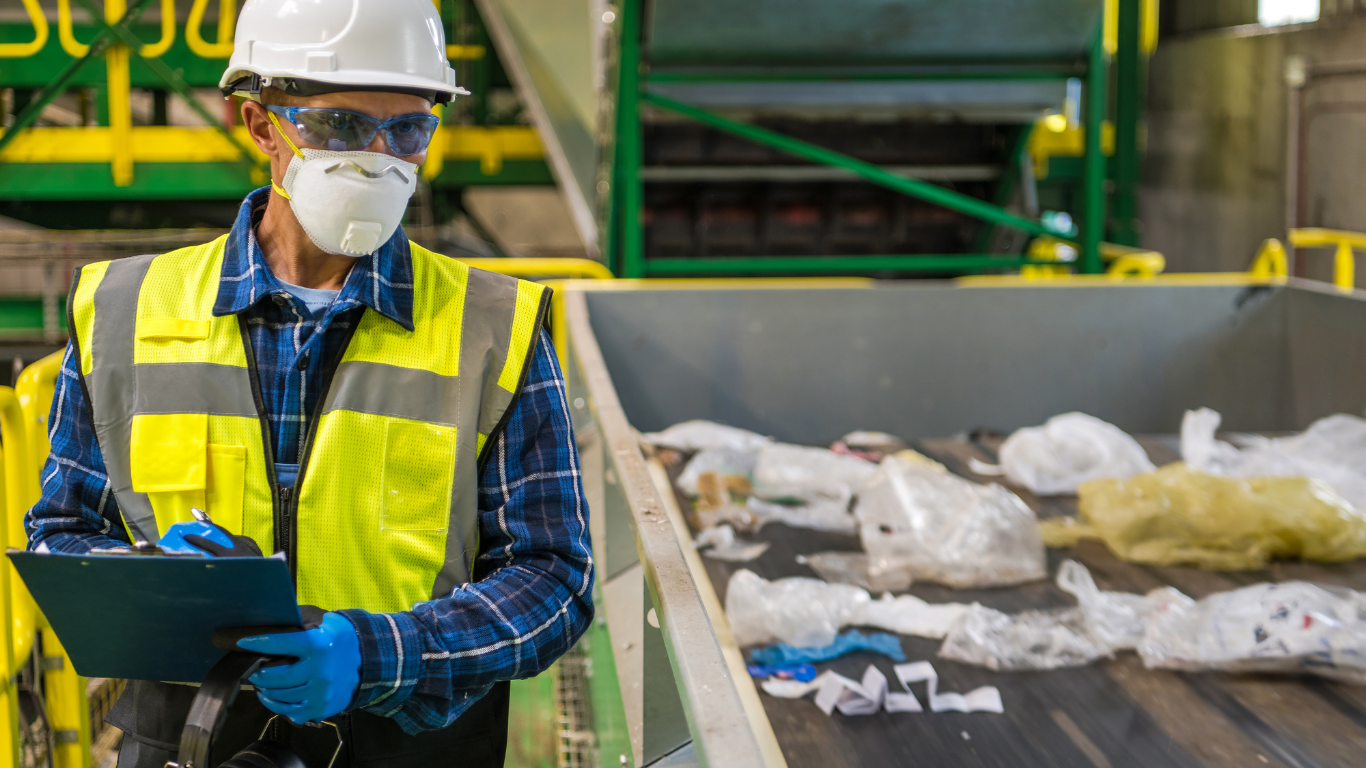
Processing efficiency isn’t just about how fast material moves through your facility, it’s about how much usable material you extract relative to what comes in. Low efficiency means higher disposal costs, lower recovery rates, and more labour hours per tonne processed.
Common efficiency losses operators should audit:
- Incorrect feed rates: Overloading or underfeeding equipment reduces throughput and increases wear, costing more per tonne processed
- Poorly calibrated sorting lines: Contamination that could be separated early becomes expensive to manage downstream
- Unoptimised compaction settings: Baler density settings that haven’t been reviewed for current material mix result in heavier loads with lower bale quality
- Manual intervention bottlenecks: Points in the process that rely on manual sorting where mechanical pre-separation would be faster and more consistent
A thorough facility assessment will identify where material is being lost, where labour hours are being absorbed unnecessarily, and where throughput is constrained. These aren’t abstract improvements, each one has a direct cost-per-tonne impact.
Resale Value: The Revenue Stream Most Operators Underestimate
The difference between a well-run and a poorly-run materials recovery operation often comes down to bale quality and commodity grade. Commodity buyers pay significantly different rates depending on material cleanliness, bale density, and moisture content, all variables that are entirely within operator control.
| Material | Low-quality grade impact | Improvement lever |
| Cardboard (OCC) | Up to 30% price reduction for contaminated bales | Pre-sort removal of wet/mixed waste |
| HDPE plastics | Rejected or heavily discounted if mixed with PET | Stream separation before baling |
| Ferrous metals | Reduced value with high organic content | Magnet separation efficiency |
| Paper grades | Downgraded if mixed with cardboard | Line calibration and operator training |
Beyond material quality, timing and buyer relationships matter.
Operators who track commodity price cycles and maintain relationships with multiple buyers consistently achieve better resale rates than those relying on a single route-to-market.
Building that optionality doesn’t require more collections, it requires better data and more deliberate commercial management of outbound material.
Equipment Uptime: The Cost You Don’t See Until It’s Too Late
Unplanned downtime is one of the most expensive things that can happen in a waste facility. A baler out of action for a day doesn’t just mean delayed output, it means backlogs, overtime, and potentially rejected loads if material sits too long.
The uptime equation:
Planned maintenance costs less than reactive repair:
Scheduled servicing of balers, shredders, and conveyor systems is consistently cheaper than emergency callout and part replacement under pressure
Wear part replacement intervals:
Running wear parts beyond their serviceable life increases energy consumption and reduces output quality before visible failure occurs
Hydraulic system health:
Pressure inconsistencies in baling equipment are an early indicator of efficiency loss; catching them early avoids major component failure
Operator-level diagnostics:
Training floor staff to identify early warning signs (unusual noise, cycle time variance, pressure drops) significantly reduces time-to-detection on developing faults
Tip: Track equipment cycle times as a routine KPI. Gradual increases in cycle time, even of a few seconds per bale, indicate wear or calibration issues that compound over a shift into meaningful throughput loss.
Quick-Reference: Cost Reduction Without Extra Collections
| Focus Area | Immediate Action | Outcome |
| Processing efficiency | Audit feed rates and conveyor calibration | Lower cost-per-tonne |
| Bale quality | Review compaction density settings | Higher resale value |
| Commodity management | Track outbound material against market rates | Better margin per tonne |
| Preventive maintenance | Schedule based on cycle counts, not calendar | Fewer unplanned stoppages |
| Staff capability | Operator training on equipment diagnostics | Faster fault detection |
The Principle Behind All of This
More collections mean more cost by definition. But a facility that’s losing material through poor sorting, underperforming equipment, or low-grade output is incurring costs just as real, they’re just harder to see on a spreadsheet.
The operators who bring cost-per-tonne down sustainably do it by treating their facility as a precision operation: tracking the right metrics, maintaining equipment proactively, and managing outbound materials commercially.
Every tonne that moves through your facility is either generating value or absorbing it. The variables that determine which way it falls are largely within your control.
Ready to Identify Where Your Facility Is Losing Value?
If your cost-per-tonne is higher than it should be, or you’re not confident you’re getting the best return on outbound material, the most useful thing you can do is get an objective assessment of what’s actually happening on-site.
Rokiwaste works directly with waste management operators to identify processing inefficiencies, improve material recovery, and reduce operating costs, without adding collections.
Get in touch with the Rokiwaste team to start the conversation.
FREQUENTLY ASKED QUESTIONS
Usually 10–25% off cost-per-tonne, through better calibration, cleaner sorting and less material loss. The key is finding where the losses actually happen first.
Absolutely. Clean, tightly compacted bales sell for more, and buyers come back to suppliers they trust.
Factor in lost throughput, overtime to clear backlogs, emergency repair fees, and disposal costs if material degrades. When operators run this calculation, the ROI on preventive maintenance becomes obvious.
Throughput against input volume. If volume is steady but costs keep climbing, look at processing efficiency or rejection rates.